

In modern lightweight composite engineering, aluminum honeycomb core density serves as the fundamental physical parameter dictating mechanical load capacity, flexural rigidity, and total sandwich panel weight. Whether designing architectural curtain walls, railway vehicle floors, high-speed marine bulkheads, or precision CNC vacuum beds, specifying the correct core density determines whether a composite assembly withstands design shear loads or suffers premature crushing failure. Understanding the mathematical relationship between cell size, foil gauge, alloy metallurgy, and nominal weight allows structural engineers and procurement specialists to optimize payload capacity while controlling material costs.
Key Takeaways for Engineers & Specifiers
Aluminum honeycomb core density is directly proportional to foil wall thickness (t) and inversely proportional to cell diameter (s), ranging from ultra-light 25 kg/m³ (1.6 pcf) to heavy-duty 120 kg/m³ (7.5 pcf).
Standard architectural cladding typically utilizes a 1/4″ to 3/8″ cell size with 0.04–0.05 mm foil (45 to 55 kg/m³), while mass transit floors and aerospace bulkheads require high-density cores exceeding 80 kg/m³.
Alloy selection (AA3003 vs. AA5052) does not alter raw volumetric weight but shifts yield compressive strength under ASTM C365 testing by up to 35%.
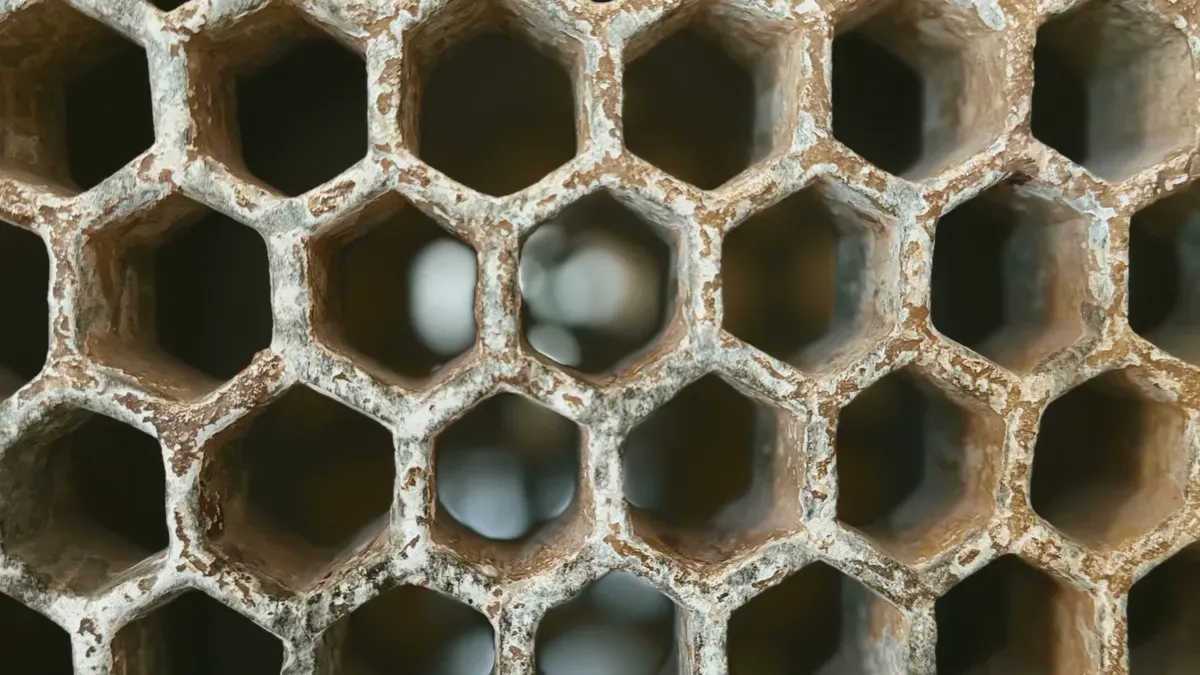
Referencing the fundamental aluminum honeycomb core structure ensures proper cell node alignment and bonding reliability prior to high-pressure lamination.
What Determines Aluminum Honeycomb Core Density?
A commercial aluminum honeycomb core consists of thin aluminum foil ribbons formed into continuous hexagonal geometries and bonded at alternating nodal intervals. Because over 90% to 97% of an expanded honeycomb block is composed of encapsulated air volume, the nominal bulk density is controlled entirely by three physical variables:
- Cell Size (s): The distance between parallel flat sides of a single hexagonal cell (commonly 1/8″, 1/4″, 3/8″, 1/2″, 3/4″ or metric 3.2 mm to 19.1 mm). Smaller cell diameters create more cell walls per unit area, resulting in higher density.
- Foil Gauge Thickness (t): The nominal thickness of the aluminum foil substrate (typically 0.03 mm to 0.08 mm or 0.0012″ to 0.0031″). Doubling the foil gauge doubles the effective weight of the core matrix.
- Base Alloy Density (ρAl): The metallurgical density of the aluminum alloy itself (approx. 2.73 g/cm³ for AA3003 and 2.68 g/cm³ for AA5052).
Honeycomb Cell Density Calculation Formula
In structural engineering calculations, the theoretical density of an expanded regular hexagonal honeycomb core is calculated using the following geometric formula:
Where t = foil thickness (mm), s = cell diameter (mm), ρAl = 2.73 × 10³ kg/m³, and Knode ≈ 1.15 accounts for the double-wall thickness at adhesive node lines and high-temperature structural adhesive mass.
Engineering Rule of Thumb: Halving the cell diameter (e.g., transitioning from 1/2″ to 1/4″) doubles the compressive strength and core density, whereas doubling the foil thickness at the same cell diameter quadruples the shear stiffness of the sandwich core.
Foil Gauge Density Chart: Metric vs. Imperial Specifications
The table below outlines nominal aluminum honeycomb core density values, foil thicknesses, and corresponding mechanical ratings evaluated in accordance with ASTM C365 (Flatwise Compressive Strength) and ASTM C273 (Shear Properties).
Alloy Influence: AA3003 vs. AA5052 Core Density & Strength
A frequent procurement misconception is assuming that aerospace-grade 5052 alloy cores are heavier than commercial-grade 3003 alloy cores. In reality, their volumetric mass is nearly identical (2.68 g/cm³ vs. 2.73 g/cm³). However, the magnesium solid-solution alloying in AA5052 delivers dramatically superior yield strength and corrosion endurance:
How to Select the Optimal Density for Your Application
Selecting an excessive core density adds unnecessary payload weight and manufacturing expense. Conversely, an under-specified core risks permanent face-sheet dimpling or core shear buckling. Use the following engineering recommendations when configuring aluminum honeycomb panel composite assemblies:
1. Architectural Building Facades & Cladding (45 to 55 kg/m³)
Exterior curtain walls undergo high negative wind suction and thermal expansion cycles. A 1/4″ cell with 0.04 mm or 0.05 mm foil provides superior flexural modulus to prevent oil-canning wave distortions across panel formats exceeding 1500 × 4000 mm, keeping panel weight under 7.5 kg/m² for complete 20 mm composite panels.
2. Rolling Stock & Mass Transit Flooring (75 to 95 kg/m³)
Train passenger floors and high-speed rail gangway partitions face localized concentrated wheel loads and foot traffic. Specifying a 1/4″ cell with 0.06 mm foil (or 3/16″ micro-cell) guarantees compressive resistance exceeding 3.5 MPa, meeting EN 45545-2 shock and fatigue requirements.
3. CNC Laser Cutter Beds & Precision Vacuum Tables (90 to 115 kg/m³)
Industrial laser cutting tables require ultra-dense 1/8″ cell micro-geometry. The dense honeycomb lattice supports small sheet metal cutouts without tipping, maintains surface flatness within ±0.2 mm, and allows uniform fume exhaust through vertical cell chambers.
Pre-Procurement Checklist: Verifying Aluminum Honeycomb Core Quality & Density Tolerances
Volumetric Density Verification: Ensure nominal density tolerance is held within ±5% of engineering data sheets.
Node Bond Integrity (Peel Strength): Node line adhesive peel strength must meet ≥ 3.5 N/mm to prevent unzipping during hot press lamination.
Slice Thickness Precision: Precision sawing tolerance must not exceed ±0.1 mm across 2000 × 12000 mm master blocks.
Surface Energy & Degreasing: Verify chemical etching or chromate conversion coating ensures water contact angle < 30° for maximum resin bonding.
Frequently Asked Questions (FAQ)
How does aluminum honeycomb core density compare to solid aluminum sheets?
Solid aluminum sheet has a fixed density of approximately 2,700 kg/m³ (168.5 lb/ft³). An aluminum honeycomb core typically ranges between 25 kg/m³ and 120 kg/m³ (1.5 to 7.5 lb/ft³), making the cellular core 22 to 108 times lighter while retaining up to 90% of the equivalent flexural stiffness in sandwich panel configurations.
Can we calculate custom honeycomb density for non-standard cell dimensions?
Yes. Custom cell geometries (including over-expanded rectangular cells for curved lamination or micro-perforated foils for acoustic applications) can be engineered precisely using the formula D = (8 / 3) × (t / s) × ρAl × Knode. Shanghai Cheonwoo Technology provides custom block slicing and density modeling to match specific structural deflection thresholds.
What is the typical compressive strength tolerance under ASTM C365?
Under ASTM C365 flatwise compressive testing, stabilized honeycomb core (with resin-bonded skins) typically exhibits 15% to 25% higher compressive yield strength than bare, unbonded honeycomb core due to face-sheet constraint of the cell wall edges. Standard production density tolerances are held within ±5%.
How does unexpanded honeycomb shipping affect delivered core quality?
Procuring unexpanded honeycomb slices (HON-SLI) reduces overseas ocean freight volume by up to 85% compared to expanded core blocks. On-site expansion using automated core pullers maintains identical post-expansion cell density and node bond shear strength, provided node line tension is calibrated to recommended pull rates.
Post time: Oct-15-2026


